I have recently finished a Remington 700 DBL pattern stock for Right Hand shooters. This pattern stock is currently at McMillan Fiberglass where they are making the mold to reproduce this stock for the open market.
Like our Legend Model 70 stocks this stock is made specifically as a Classic Sporting Weight hunting stock. It features a straight comb with .550 drop at the comb nose and .550 at the heel. The butt is made with "CAST OFF" at both the toe and heel and comes out of the mold with a standard 14" length of pull. Unless special ordered specifically these will be machine inletted as Custom Drop In for the BDL Remington OEM factory or Williams Rem-700 steel floor plate and trigger bow assembly.
Unless otherwise requested these stocks will be sold without the ejection port or bolt notch installed to lend more versatility to this stock for a broader spectrum of 700 clones now on the market. While this stock was made specifically for the Long and Medium length 700 actions it will work very well with the Borden and Defiance actions as long as the rear tang is machined like the original 700. The stock will not come with swivel studs, recoil pads or painted and this service is not offered.
I anticipate the mold to be finished in 90 days and stocks available for sale by early to mid summer. I will take pre-production orders but will not accept down payments for these order. For further information please contact me 435-755-6842 9am-5pm. MST or by e-mail echolslegend@comcast.net
Monday, January 27, 2014
Tuesday, January 21, 2014
Given A Choice
From time to time I am asked if I were to build a rifle for myself just how would I assemble the package. My answer is usually met with a raised eyebrow and a pause. I have suggested my approach to what I consider the ideal magazine rifle many times over the years and yet only a handful of clients have signed off on the plan.
1. It would be built for either scope or iron sight use, not for both. At 56 I'll take the scope every time for the type of hunting I currently do or will likely do in the foreseeable future. Detachable mounts ? No thanks I find it hard enough to keep a scope immobile.
2. The bolt would always be swept to the rear and positioned low enough to allow the bolt handle to clear the ocular lens mounted a close as possible to the centerline of the bore. The knob would always be checkered.
3. I am not a fan of bantam feather weights, I'll leave it at that.
4. The stock would not have an Ebony tip. Why cut of $130 worth of stable french walnut to install $20 worth of Ebony. As they are dissimilar materials by nature the expansion and contraction rates will soon be different.
5. The butt will always be fit with a natural rubber recoil pad without a widows peak. It would be 1" thick and always red in color. No leather covering, no toe and heel plates, no checkered steel, no skeleton butt plates. I want non skid rubber thank you.
6. The swivel bases I use on my Classics were developed by the late Tom Burgess. However I do not shape a platformed border around the swivel base. Rather I contour the steel base to match the contour of the stock. The swivel can't ever twist in the stock.
7. The barrel would be tastefully free floated.
8. It would have a 24 LPI open point checkering pattern.
9. All the guard screws would be engraved Allen heads and surrounded by aluminum pillars. All the scope base and rings screws would be 8x40's with T-15 Torx heads.
10. All the metalwork would be Caustic blued. Not rust blue, not Cera-kote, not MP3.
Below is such a rifle. This 5 shot, Left Handed Model 70 is chambered in 404 Jeffery and follows the parameters listed above with the exception of the Recoil Pad which does have a widows peak.
I have always felt a rifle build in this manner is the epitome of simplistic elegance.
Studio Photo's by Kevin Dilley Kevin@klikphoto.net
Swivel Base pic supplied by LB
Tuesday, January 7, 2014
A Walk In The African Sun
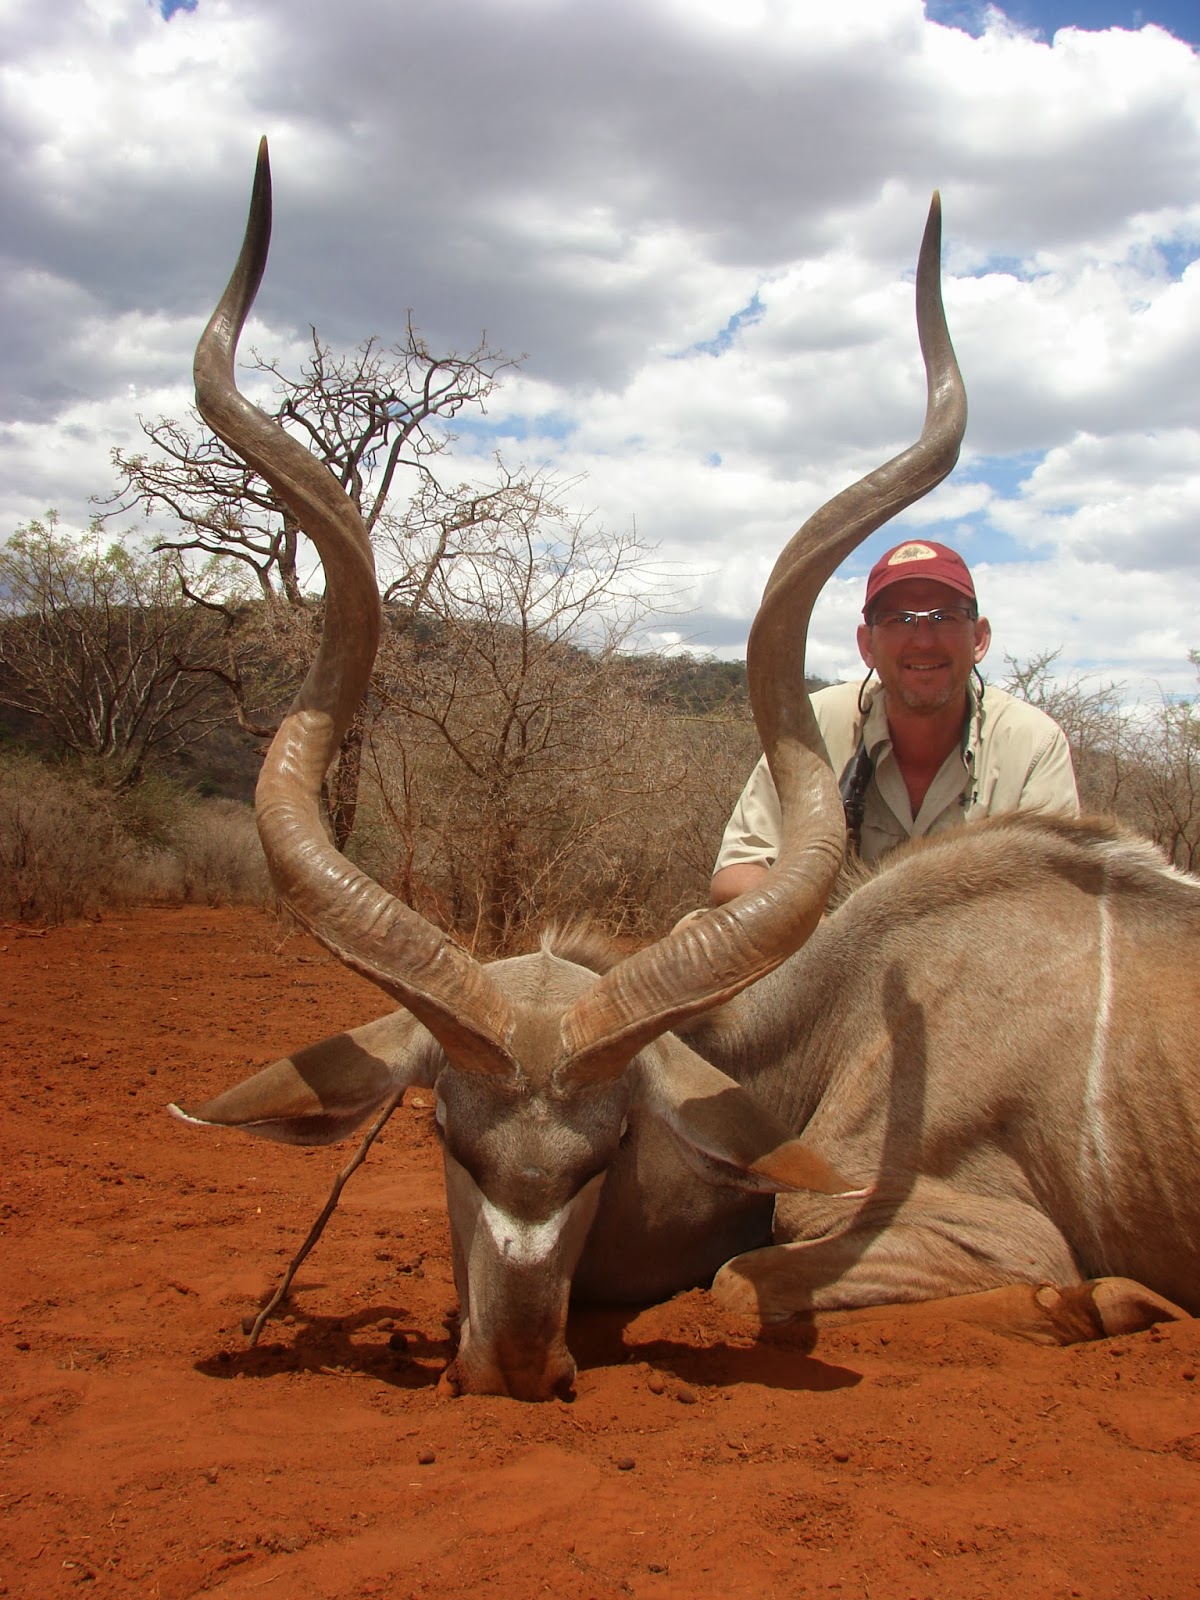
Terry Niegel sent in a few pictures from his recent safari in Namibia and South Africa. Terry's PH for this hunt was Bobby Hansen (Bobbyhansensafaris.com.) This was Terry's 2nd hunt with Bobby. The plan for this hunt was to visit a new area in Africa, hunt as hard as they could from dawn until dusk and roll with the punches. To say they did OK is a bit of an understatement. Terry used his Legend Sporter chambered for 300 H&H. This rifle has been his go-to rifle for quite some time. Loaded with 168gr TTSX's it has become the long arm of the law on any ridge-line that he settles down to glass from. The bluing is now worn silver in many places and the recoil pad needs replacing. A visible testament to its use.
Their joint persistence and luck ran deep as the wide-glide Kudu bull is stunning from any angle, the second bull more typical and equally impressive. The Mountain Zebra and Gemsbuck added sweat equity to the mix. The Eland is a stunner in anyones book, this old bull is a once of a life time encounter, long and worn, a true desert ghost. No one had ever seen this bull in the area, Bobby had been there for three previous weeks, the staff lives there but no one had a glimpse, not a hint, just an apparition that appeared out of the thorns.
Instead of electing to fly from Namibia to the Limpopo River area of South Africa to do some additional hunting. Terry elected to drive the 27 hours to the Limpopo with Bobby. While the drive was long the scenery was always changing. Dusty and dry they rolled into the Limpopo just in time for dinner and a sun downer.
In the remaining days of the trip they took a nice Bushbuck among the islands and pools in the river bed. While the quality a hunt should never be judged on the number of animals taken on many levels I think we can could call this trip a roaring success.
Tuesday, December 10, 2013
You Just Can't Make This Stuff Up
In my last post I mentioned we had just received a Fisher Barrel Vise. Well, today we actually had to put it to use. We had been shipped a very clean Pre-64 Super Grade 375 H&H to do some minor work to. Unfortunately the rifles bolt came loose in the case and the US Postal Service must have used the gun case as a temporary truck ramp while it was in transit and some serious cosmetic damage occurred. As the barrel needed to be removed Brian went through the normal SOP with our current barrel vise that has been a mainstay in my shop for over 24 years.
Throughout the years we have run into a few barrels that the only way we could remove those barrels was to place the barreled actions in our lathes 3 jaw chuck and by using a parting tool right up against the receiver face cut a groove to the minor thread diameter into the barrel. By doing so this reduced the shoulder tension and allowed the barrels to removed but this method destroys the barrel. Fortunately all those barrels were to be replaced anyway.
The circumstance we faced this morning was quite different, this barrel had to be removed, re-blued and reinstalled. All Brian's attempts did not break the action free from the barrel. He finally threw up his hands and backed away from the task to re-group, an uncommon occurrence I can assure you. What I saw was a perfect time to remove our old vise and set the Fisher in place. This required a trip to town for some additional hardware and the relocation of a mounting hole. In short order the Fisher was in place. The Winchester barrel shank OD was approximately 1.245 and the bushing that Jerry had sent along had an ID of 1.250. I found and placed a .004 thick piece of card stock around the barrel shank, slid the bushing halves over the card stock then transferred the barrel and bushing into the vise. Since the upper jaw is spring loaded the installation of said barrel was painless.
Then I snugged down all four 3/4" bolts that lock down the bushing and barrel. This was done with a socket wrench. My old vise only used two screws to hold down the top vise jaw. The action wrench was then re-installed. I gave the action wrench a smart thud with a dead blow hammer and the action spun free from the barrel. It was just that simple. The vise is now paid for.
Now tell me, who writes these scripts ?
Friday, December 6, 2013
Jerry Fisher Barrel Vise Arrives
I picked up my new Jerry Fisher barrel vise at the Post Office today and later in the afternoon I opened the box and gave this tool the hairy eyeball. Visually it is apparent the vise was made by a talented machinist. The exterior and interior finish is excellent, the tolerances are tight. A class act in anyones book.
One noticeable feature is the upper jaw of the vise is spring loaded and as you release the tension on the four 3/4" hex nuts
The upper jaw rises approximately .150 away from the lower base jaw. A damn handy feature when you're assembling a newly blued barrel and action as it gives you an ample margin of clearance to install and remove these freshly blued components without requiring a third hand to prevent marring the parts in the procedure.
A selection of aluminum barrel shank bushings are available from Mr. Fisher in a variety of common barrel shank sizes. Or you can make your own from standard 2" Aluminum or Micarta round stock.
The cost of the vise is $575.00 which I think for a one time investment is not expensive at all over the length of ones career. Good tools demand a fair price and are made to last. I have little doubt this vise will be a good addition to the shop.
Sunday, November 17, 2013
458 Lott Legend And The Trijicon RMR06 Sight System
Over the last year we have had a number of inquires in regard to the Trijicon RMR sights and if they could be applied to our rifles? The questions we had seemed to work themselves out and I modified 2 Trijicon RM62 gunsmith bases that we finally acquired after quite a bit of effort to locate. The height of the stocks comb in relation to the height of the sight itself is as important as any other sight system. The Legends stock design and the RMR06 do work well together.
Anders arrived in Utah to hunt Mule Deer as well as have further work done to his Legend Heavy Sporter chambered for 458 Lott. This rifle has been used on one Elephant hunt already where he used both our Peep Sight and a S&B Zenith mounted in a set of our 30-mm rings. He did in fact use both sight systems to take two different Elephants. In short to try them both under field conditions.
One of his latest desires was to install the RMR06 as yet a third option. As we keep detailed records of scope mounts we make for each project I was able to duplicate the same radius that Brian had surface ground on the front ring to the underside of the RMR base, locate and drill the counterbores for the 8x40 screws and then have the base blued and ready for assembly when he stepped off the plane from Sweden. It took longer to drive to the range than it took to zero in the RMR06. He shot approximately 20 rounds to zero and test the system. He plans to use this rifle this winter in Sweden to add some wild boar to the menu for the holidays.
The Union Club In New York City Echols & Company Presentation
Last week I gave a Power Point Presentation to the Union Club In New York City. This presentation gave those in attendance a behind the curtain view of the construction process used to build both our Classic and Legend Rifles. My host Richard Turnure, club members, invited guest and the staff at the Union Club were most gracious and made my short stay quite memorable. This institution is steeped in history and it was an honor to be there. I have given these presentations all over the country for 20 years and find these engagements very enjoyable.
The last time I was in Manhattan was in 1979 when I applied for a position at Griffin & Howe. At the end of a two day interview I was offered a job but ultimately declined the position.
I would like to thanks those that were in attendance and hope the material covered was of interest to everyone.
The last time I was in Manhattan was in 1979 when I applied for a position at Griffin & Howe. At the end of a two day interview I was offered a job but ultimately declined the position.
I would like to thanks those that were in attendance and hope the material covered was of interest to everyone.
Photo credit thanks to Wikipedia
Subscribe to:
Posts (Atom)